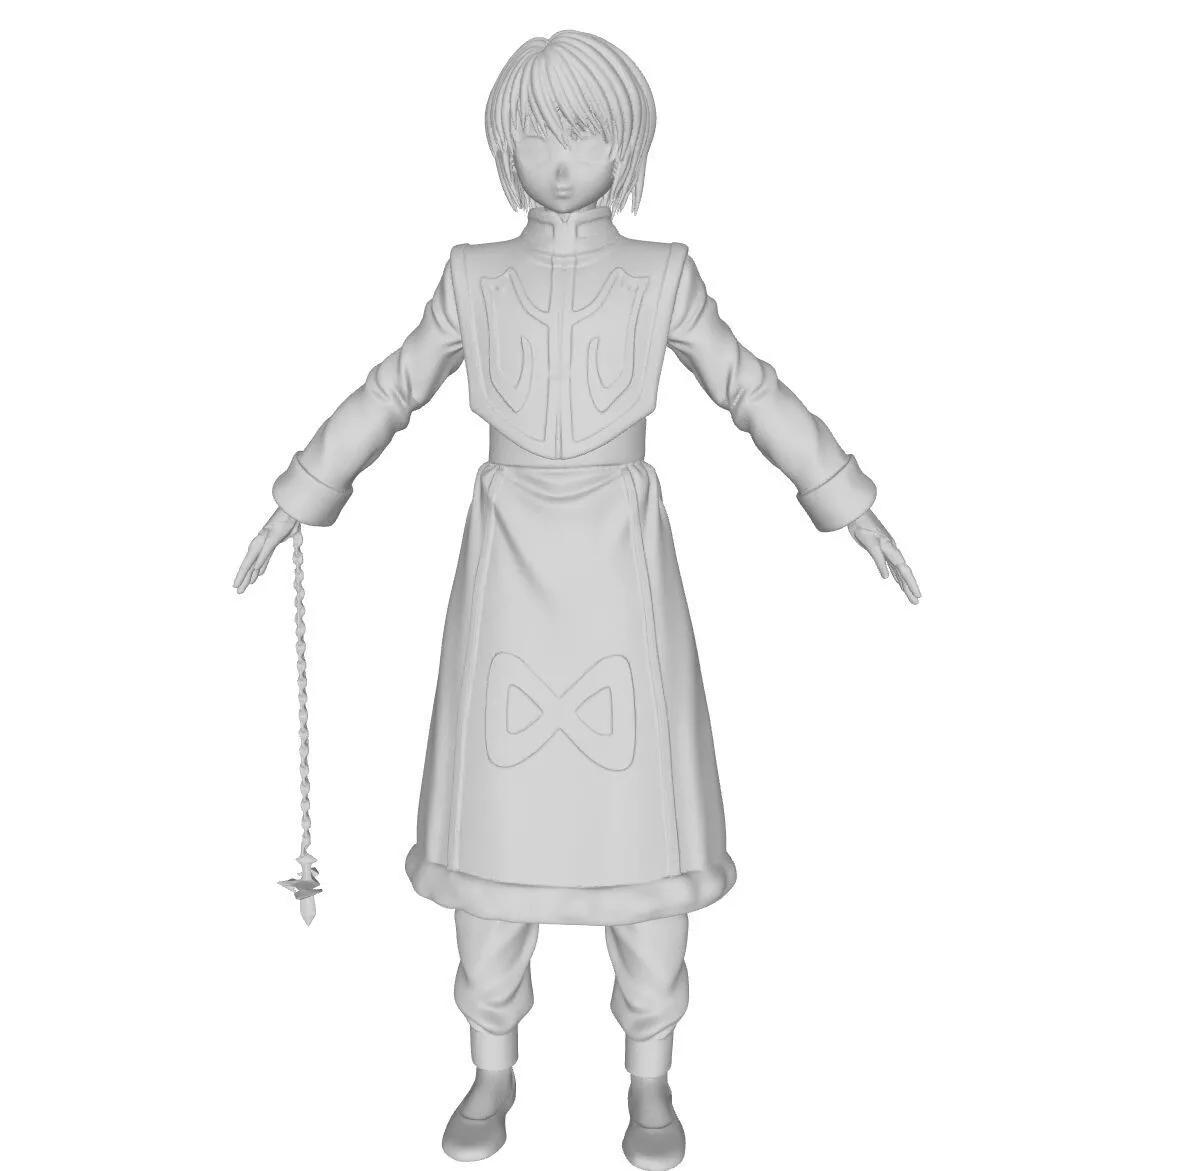
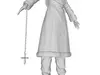
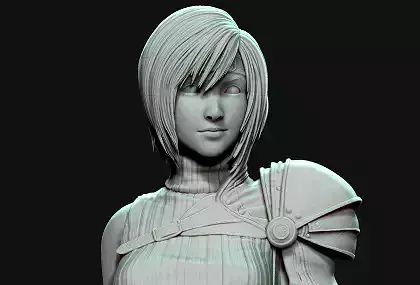
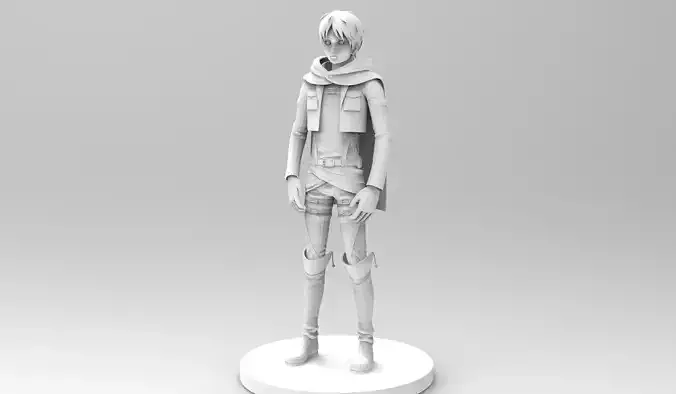
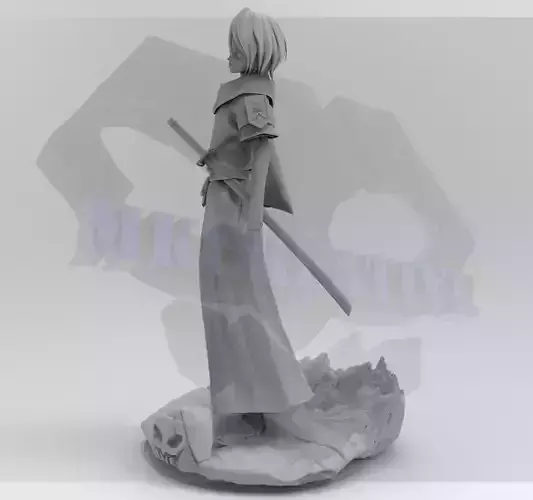
High-detail STL model of Kurapika from the anime and manga series Hunter x Hunter. This figurine features his iconic long white tabard, short hair, and signature chain weapon held in his right hand.
The model is scaled to approximately 130mm in height, making it ideal for desktop display or cosplay prop reference. The sculpt includes detailed clothing folds, layered sleeves, and the chain dagger accessory.
Optimized for both FDM and resin 3D printing. Supports are recommended for the arms, hair tips, and chain weapon. The model is provided as a single solid mesh in standard STL format.
TECHNICAL SPECS
- Format: STL
- Units: Millimeters (mm) — IMPORTANT: Model is authored in centimeters. Scale by 10x (1000%) in your slicer to convert to true millimeters.
- Dimensions: 75 x 26 x 120 mm (after scaling)
- Vertices: 349,652
- Faces: 698,917
- Topology: Manifold, Watertight, print-ready
- Structure: Single-piece solid model (not split)
PRINTING INSTRUCTIONS
Printer TypeFDM (Fused Deposition Modeling) is fully supported. Recommended printers: Bambu A1, Creality Ender series, Prusa MK4, or equivalent. For maximum facial and hair detail, Resin (SLA/DLP/LCD) is strongly recommended. FDM will produce slightly softer features on fine details such as fingertips and hair strands.
ScaleThe model is saved in centimeters. Before slicing, apply a uniform scale of 10x (1000%) in your slicer to convert to millimeters. Final height after scaling is approximately 120 mm.
Supports — REQUIREDAdd supports under the hair strands, sleeves, coat hem, chain weapon, and fingertips to ensure clean overhangs.
Type: Auto-generated
Overhang Angle: 50 degrees
Density: 0.25 – 0.30
Top Distance: 0.2 – 0.3 mm for easy removal
Use Tree Supports if your slicer supports them
Brim / Bed AdhesionEnable Brim for reliable bed adhesion. Strongly recommended for tall, thin models and small base contact areas. Skirt alone is insufficient.
Layer Height
Standard quality: 0.20 mm
High detail: 0.16 mm
Maximum recommended: 0.20 mm
Infill (FDM only)15% – 20%
Wall Thickness / Perimeters (FDM only)3 – 4 perimeters
Nozzle Temperature210 – 220 degrees Celsius (for PLA+)
Bed Temperature60 degrees Celsius
OrientationPrint upright with a wide base. Ensure the model is stable and well-supported from the base up. Do not tilt on FDM; keep the base flat on the build plate.
Slicer Workflow (Kiri:Moto / Cura / Bambu Studio)
Import the STL file
Scale: Multiply by 10 (x10) to convert from centimeters to millimeters
Set Layer Height: 0.16 – 0.20 mm
Configure Supports: Auto, 50 degree angle, 0.25 density
Enable Brim (8–10 lines minimum)
Preview the slice to verify supports cover all overhangs
Export G-code and print
POST-PROCESSING (FDM)
- Remove Supports: Use flush cutters carefully, especially around the hair, chain weapon, and fingers.
- Sand: Start with 400 grit, then 800, then 1200 grit to smooth layer lines.
- Prime: Apply a grey or white primer coat.
- Paint: Use acrylic paints with a fine brush or airbrush.
- Finish: Apply a clear coat (glossy or matte) for protection.
POST-PROCESSING (Resin)
- Wash: Rinse in IPA 95% for 3–5 minutes to remove excess resin.
- Cure: Expose to UV light for 2–5 minutes.
- Remove Supports: Use flush cutters carefully.
- Sand, prime, paint, and finish as above.
IMPORTANT NOTES
- Do not attempt to print without supports — the hair, sleeves, and chain weapon will fail.
- This is a high-detail model (700K faces). Slicing may take longer than usual.
- The model consists of 237 connected surface groups within a single solid shell. No assembly is required; it prints as one continuous piece.
- Facial details and fingertips may appear slightly soft on FDM. Resin printing is recommended for customers seeking maximum detail.
- Always verify scale before printing. Failure to scale by 10x will result in a 12 mm tall print.